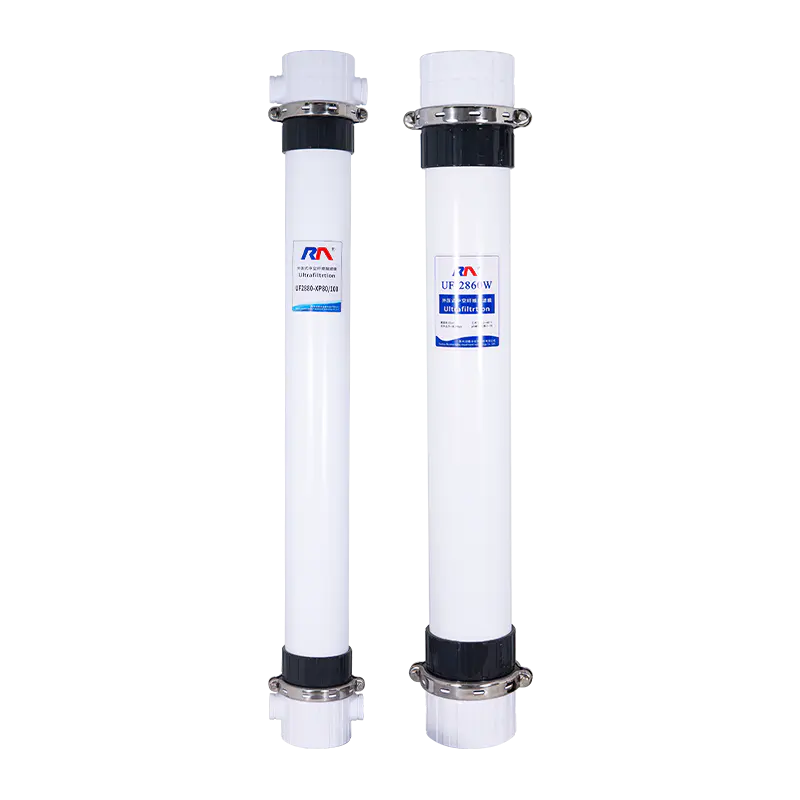
Industrial facilities worldwide face mounting pressures to optimize water consumption while complying with strict environmental discharge limits. Modern manufacturing operations rely heavily on sophisticated filtration hardware to purify impaired water sources efficiently. Selecting a reliable reverse osmosis membrane manufacturer helps facility operators secure high-performance components tailored to unique factory requirements. Understanding the fundamental science behind modern separation modules empowers engineers to maximize system longevity and reduce ongoing operational expenses.
Fluid Dynamics and Thermodynamic Principles
Pressure-driven filtration relies on applying external mechanical force to overcome natural osmotic equilibrium within saline solutions. Specialized semi-permeable barriers allow pure water molecules to pass through while trapping dissolved mineral ions and organic particles. Managing cross-flow velocities across active filtration layers prevents localized concentration polarization from damaging fragile composite materials. Plant technicians monitor operating pressure differentials closely to maintain optimal hydraulic throughput during continuous production shifts.
Balancing feed water velocity with membrane permeability maximizes liquid recovery rates without triggering accelerated surface scaling events. Technical design specifications dictate that fluid distribution channels must remain clear of physical obstructions to ensure uniform flow distribution. Proper hydrodynamic management extends component lifespans significantly across demanding municipal and industrial fluid processing environments.
Polymer Composition and Thin-Film Technology
Advanced composite manufacturing protocols utilize sophisticated polyamide chemistry to construct durable, high-flux semi-permeable barrier layers. Interfacial polymerization techniques create ultra-thin active surfaces that maximize pure water permeability while blocking unwanted ionic species effectively. Selecting appropriate polymer matrix formulations determines the long-term chemical resistance and structural integrity of separation elements.
Rigorous quality control during production ensures uniform pore distribution networks across every individual membrane sheet. These microscopic structural optimizations allow facility operators to maintain high desalination performance even under fluctuating feed water conditions. Material science innovations continue to bridge the gap between high productivity and low energy overhead in modern filtration systems.
Pretreatment Protocols for Saline Feed Streams
Raw water extracted from surface reservoirs or municipal grids frequently contains suspended silt and microscopic organic matter. Inadequate pretreatment protocols often trigger rapid particulate fouling and irreversible membrane channel blockage within high-pressure loops. Industrial operators deploy multi-barrier clarification trains to protect delicate secondary separation modules from premature physical damage.
Analyzing silt density indexes daily verifies that incoming fluid meets strict manufacturer inlet quality criteria before processing. Comprehensive pretreatment stabilizes overall plant performance and shields sophisticated polymer elements from unexpected chemical shock. Robust upstream protection secures continuous high-pressure performance across demanding factory operating environments.
Applications in Municipal Water Supply Systems
Municipal authorities manage vast distribution networks that must supply safe drinking water to growing urban populations daily. Surface water reservoirs and underground aquifers frequently require advanced clarification before reaching public distribution pipelines. Synthetic separation modules remove suspended pathogens, natural organic matter, and microscopic turbidity efficiently without adding harmful chemicals. Public utility engineers rely heavily on robust filtration networks to safeguard community health across urban regions.
Inland cities increasingly look toward brackish groundwater sources to supplement declining freshwater reservoirs and municipal supplies. Processing moderate-salinity feeds demands reliable separation hardware capable of handling variable ionic concentrations daily. Large-scale public utility projects depend on custom-engineered filtration units to transform impaired water into potable public resources.
Industrial Wastewater Reclamation and Reuse Strategies
Industrial manufacturing plants generate complex wastewater streams containing aggressive solvents, heavy metals, and high concentrations of dissolved salts. Environmental regulations compel factory operators to treat industrial effluent thoroughly before discharging liquid waste into local waterways. Advanced membrane separation technologies enable facilities to recover valuable chemical byproducts while concentrating residual waste streams. Effective reclamation practices help plants comply with strict zero liquid discharge environmental mandates.
Managing difficult industrial wastewater requires durable polymer materials capable of withstanding harsh chemical cleaning solutions safely. Specialized filtration components resist oxidative degradation when exposed to aggressive disinfectants during routine maintenance washing cycles. Industrial processors achieve long-term environmental compliance without compromising daily manufacturing productivity.
Power Generation and Boiler Feed Protection
Thermal power stations consume massive volumes of water to generate high-pressure steam that drives electricity turbines. Mineral-laden boiler feed water causes hazardous scale deposition on internal turbine blades, reducing overall plant operational efficiency. Power plant operators deploy sophisticated desalination hardware to remove calcium, magnesium, and reactive silica before water enters boilers. Preventing mineral scaling protects heavy-duty infrastructure from premature mechanical failure and costly downtime.
Closed-loop cooling towers also require continuous side-stream filtration to manage suspended solid accumulation and mineral concentration. Industrial engineers design robust pre-treatment trains to safeguard primary steam generation equipment against thermal shock. Reliable separation technology supports uninterrupted electrical power generation across regional energy distribution networks.
Economic Benefits and Operational Cost Savings
Adopting advanced separation technologies yields substantial financial savings for large-scale industrial operations and municipal infrastructure projects. Optimizing fluid recovery rates reduces raw water intake volumes and minimizes expensive wastewater disposal fees significantly. Furthermore, durable polymer modules lower replacement frequencies, thereby conserving capital expenditure budgets over extended operational lifespans.
Financial efficiency remains a primary driver behind the widespread industrial adoption of modern membrane filtration systems. Project developers allocate saved financial resources toward broader facility automation and environmental monitoring upgrades. Lower maintenance overhead combined with reduced chemical consumption improves the overall economic viability of commercial water treatment plants.
Selecting the Right Component Supplier
Sourcing dependable filtration components requires careful evaluation of manufacturing capabilities, technical support, and product customisation options. Industrial buyers look for partners who understand complex water quality challenges across diverse manufacturing sectors. A qualified reverse osmosis membrane manufacturer provides tailored solutions that address specific salinity profiles and flow requirements. Collaborating with experienced technical teams ensures seamless integration and long-term operational success for water treatment projects.
Evaluating vendor credentials involves assessing research and development strength, patent portfolios, and customer service responsiveness. Industrial facilities benefit immensely from working with established production bases that maintain strict quality control standards. Comprehensive technical consulting minimizes deployment risks and accelerates the timeline toward full commercial production capacity.
Conclusion
Modern water treatment demands innovative separation science and dependable filtration hardware to satisfy strict environmental standards. Working with an experienced reverse osmosis membrane manufacturer provides facility managers with the tools needed to overcome complex water scarcity challenges.
At Runmo, we specialize in the technical development and production of high-performance reverse osmosis membranes, ultrafiltration membranes, and specialized polymer membranes. Our extensive product catalog serves municipal water supply, industrial wastewater reuse, chemical processing, electronics, and pharmaceutical sectors globally. Reach out to our engineering department today to discuss custom membrane configurations for upcoming municipal or industrial projects.